logo
Supal (Changzhou) Precision Tools Co.,Ltd
Sobre nós
O seu parceiro profissional e confiável.
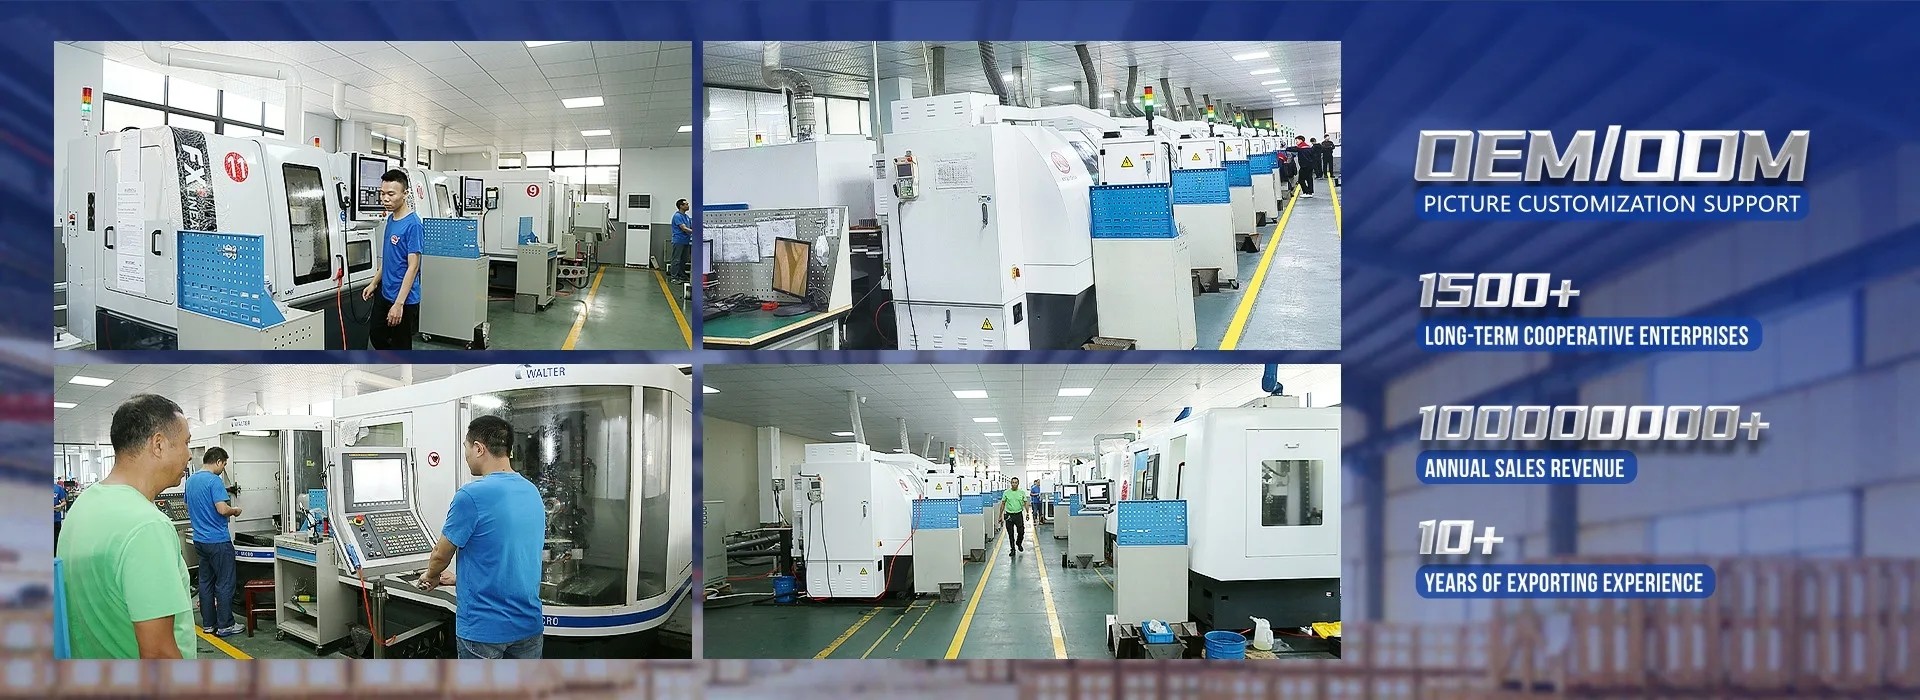
Supal (Changzhou) Precision Tools Co., Ltd. está envolvida no design, produção e comercialização de ferramentas de metal duro para muitos anos, com um investimento total de mais de 10 milhões, e é composta por um grupo de funcionários experientes.Como fabricante profissional de ferramentas, tornou-se um dos membros diretores da Changzhou Xiaxiashu Tools Association. A empresa introduziu máquinas Walter e Schutte da Alemanha, ANCA da Austrália e retificadoras de cortadores NC de cinco eixos; além ...
Aprenda mais

0

Ano estabelecido:

0

Milhão+
Empregados

0

Milhão+
Vendas anuais:
CHINA Supal (Changzhou) Precision Tools Co.,Ltd Alta Qualidade
Selo de confiança, verificação de crédito, RoSH e avaliação da capacidade do fornecedor. A empresa tem um rigoroso sistema de controlo de qualidade e um laboratório de teste profissional.
CHINA Supal (Changzhou) Precision Tools Co.,Ltd DEVOLVIMENTO
Equipe interna de projeto profissional e oficina de máquinas avançadas. Podemos cooperar para desenvolver os produtos de que necessita.
CHINA Supal (Changzhou) Precision Tools Co.,Ltd Fabricação
Máquinas automáticas avançadas, sistema estritamente de controlo de processos. Podemos fabricar todos os terminais elétricos além da sua demanda.
CHINA Supal (Changzhou) Precision Tools Co.,Ltd 100% SERVIÇO
Embalagens a granel e pequenas embalagens personalizadas, FOB, CIF, DDU e DDP. Deixe-nos ajudá-lo a encontrar a melhor solução para todas as suas preocupações.

Qualidade Ferramentas de moagem de carburo & fresas de topo quadradas Fabricante

Encontre os produtos que melhoram para cumprir suas exigências.
Casos e Notícias
Os Últimos Pontos Quentes.
Desgaste Irregular da Flauta em Fresas de Metal Duro: Causas e Solução de Problemas
Desgaste irregular do canal em fresas de topo de metal duro: causas e solução de problemas Uma fresa de topo de metal duro pode apresentar desempenho aceitável em um canal e desgaste anormal, lascamento ou aresta postiça em outro. Essa condição irregular é muitas vezes atribuída à qualidade inconsistente do metal duro, mas o padrão frequentemente aponta para desvio, fixação da ferramenta, fixação da peça, engate ou vibração. Quando um canal suporta mais carga de corte, a ferramenta pode falhar precocemente, mesmo que a velocidade e o avanço programados pareçam razoáveis. Para maquinistas CNC, engenheiros de processo e engenheiros de compras, o desgaste irregular do canal é uma valiosa evidência de diagnóstico. A localização e distribuição do desgaste podem ajudar a distinguir um problema de ferramenta de um problema de configuração. Uma investigação prática deve, portanto, examinar a ferramenta usada, o suporte, a máquina, a peça, o percurso da ferramenta, o formato do cavaco e os dados de corte em conjunto, em vez de substituir a ferramenta sem identificar o desequilíbrio de carga. Este guia explica as causas comuns do desgaste irregular do canal em fresas de topo de metal duro, como interpretar o padrão de desgaste e como estabelecer uma sequência de correção controlada. Como é o desgaste irregular da flauta O desgaste irregular significa que os canais não compartilham o trabalho de corte de maneira razoavelmente consistente. A diferença pode aparecer como: Uma flauta com desgaste de flanco visivelmente mais pesado Lascamento concentrado em uma aresta de corte Material acumulado preso a apenas uma flauta Arredondamento de arestas diferente de flauta para flauta Uma faixa brilhante em uma flauta e marcas de corte normais em outra Marcas de vibração que correspondem a uma seção sobrecarregada da ferramenta Uma perda repentina de acabamento ou estabilidade dimensional após um curto ciclo de corte A ferramenta deve ser inspecionada sob iluminação consistente e, quando disponível, ampliação. Registre qual canal apresenta maior desgaste, onde o dano começa ao longo do comprimento de corte axial e se o padrão se repete em diversas ferramentas da mesma configuração. Uma única flauta danificada não prova que a ferramenta foi fabricada incorretamente. Se a mesma posição do canal falhar repetidamente no mesmo suporte ou máquina, a configuração se tornará uma fonte mais provável de carga irregular. A causa mais comum: esgotamento Por que o runout sobrecarrega uma flauta O desvio radial evita que todos os canais removam cavacos da mesma espessura. Uma flauta pode envolver mais fortemente enquanto outra flauta remove pouco material ou fricção. O canal sobrecarregado sofre maior estresse mecânico e térmico, o que pode levar a desgaste acelerado, lascamento ou aresta postiça. O desvio pode ocorrer no fuso, no suporte, na pinça, na porca da pinça, na haste da ferramenta ou na superfície de assentamento da ferramenta. Também pode ser amplificado por uma projeção longa ou por uma interface danificada. Um pequeno valor de desvio pode representar uma porcentagem significativa de uma ferramenta de pequeno diâmetro, portanto a condição aceitável depende do diâmetro da ferramenta e da aplicação, e não de um único número universal. Uma verificação prática de esgotamento Use o método de medição normal aprovado e inspecione o mais próximo possível da aresta de corte. Antes de medir, limpe a haste da ferramenta, a pinça, a porca, o cone do suporte e a interface do fuso. Confirme se a ferramenta está assentada corretamente e se os componentes do suporte não estão desgastados ou danificados. Não utilize uma redução de parâmetro como substituto para a correção de desvio inaceitável. Abaixar o avanço pode reduzir a carga média, deixando o mesmo canal sobrecarregado a cada rotação. Problemas de fixação e assentamento de ferramentas Contaminação e superfícies de contato danificadas Uma pequena lasca, rebarba, película de óleo ou partícula entre a haste e a pinça pode inclinar a ferramenta. O resultado pode ser um carregamento desigual do canal, mesmo quando o suporte parece apertado. Inspecione as superfícies de contato durante cada troca de ferramenta e siga o procedimento de limpeza. Condição da pinça e do suporte Uma pinça desgastada pode aderir de forma desigual ou não conseguir apoiar a haste concentricamente. Uma porca de pinça, suporte cônico ou interface do fuso danificados podem criar sintomas semelhantes. Se diversas ferramentas apresentarem o mesmo padrão de desgaste de canal único, teste o suporte com uma ferramenta estável conhecida ou mova a operação para um suporte verificado antes de alterar a geometria da ferramenta. Projeção excessiva A deflexão da ferramenta aumenta com a projeção. Uma ferramenta longa pode se afastar do caminho programado, especialmente durante um corte radial pesado ou quando a peça não é rígida. A deflexão altera o engajamento real e pode fazer com que uma área da ferramenta trabalhe mais do que o esperado. Para recursos profundos, use a ferramenta prática mais curta. Se o alcance estendido for inevitável, considere o equilíbrio entre geometria e rigidez oferecido peloFresas de pescoço longo, e valide a configuração completa em vez de assumir que uma ferramenta mais longa pode usar os mesmos dados de corte que uma ferramenta curta. Percurso e efeitos de engajamento Engajamento desigual nas esquinas Uma ferramenta pode sofrer uma carga maior nos cantos, entradas, saídas ou alterações no engate radial. Se o mesmo canal atingir repetidamente a seção de carga mais alta devido ao desvio ou à orientação do percurso, o padrão de desgaste pode se tornar fortemente assimétrico. Revise o engate radial e axial programado no local onde o dano começa. Compare a simulação CAM com a peça real, incluindo variação de material, revestimento fundido, furos cruzados e áreas interrompidas. Corte e ranhura em largura total O engate em toda a largura aumenta a carga radial e deixa menos espaço para os cavacos escaparem. Se houver excentricidade, o canal sobrecarregado também poderá encontrar cavacos compactados, aumentando a chance de lascamento e aquecimento. Quando o recurso permitir, avalie uma estratégia de engate radial inferior ou passes separados de desbaste e acabamento. Choques de entrada e saída Um mergulho abrupto, uma saída sem suporte ou uma mudança repentina no engate podem criar um impacto que danifica um canto ou flauta. Se a ferramenta falhar imediatamente após a entrada, inspecione o método de entrada, o suporte da peça e a condição real de entrada antes de trocar o revestimento. Fixação de trabalho e rigidez da máquina O desgaste irregular do canal pode originar-se fora da ferramenta. Uma peça que se move, uma parede fina que desvia ou um acessório com suporte inadequado alteram a carga de corte durante o passe. A ferramenta pode então alternar entre fricção e impacto, produzindo um padrão de desgaste irregular. Verifique o contato do dispositivo, a força de fixação, o suporte sob seções finas e a rigidez da corrente máquina-ferramenta-peça. Ouça a mudança no som à medida que a fresa se move pelas diferentes áreas da peça. Se o desgaste estiver concentrado onde a peça tem menos suporte, a fixação pode ser a correção primária. O Chatter também pode sobrecarregar arestas selecionadas. Um passo variável ou outra geometria de controle de vibração pode ajudar em uma aplicação adequada, mas não pode substituir a correção de balanço excessivo, desvio, fixação fraca ou um percurso de ferramenta instável. Considerações sobre materiais, geometria e revestimento Combine a ferramenta com a peça de trabalho A geometria da ferramenta deve refletir o comportamento de formação de cavacos, dureza, tendência de adesão e nível de interrupção do material. Uma aresta afiada pode suportar um cisalhamento limpo em um material propenso a aderência, enquanto uma preparação de aresta mais tenaz pode ser mais adequada onde predomina o impacto ou o desgaste abrasivo. Ao compararFerramentas de fresagem de metal duro, revise a contagem de canais, a hélice, a resistência do núcleo, a preparação da borda, o substrato e o revestimento como um sistema. É improvável que uma mudança de revestimento por si só corrija a sobrecarga de um canal causada pelo desvio. O revestimento segue o mecanismo de falha A seleção do revestimento deve ser baseada no modo de falha dominante. A adesão, o desgaste térmico e a abrasão requerem estratégias diferentes. Se um canal apresentar material soldado enquanto outro apresentar fricção, primeiro investigue a carga desigual e a formação de cavacos. Se o revestimento lascar uniformemente nas bordas encaixadas, as condições térmicas ou de adesão poderão merecer mais atenção. Qualquer recomendação de revestimento ou geometria deve ser tratada como uma referência inicial e validada na máquina real, suporte, fixação, método de refrigeração e classe de material. Quando a geometria personalizada é justificada Uma ferramenta padrão pode não fornecer a combinação necessária de alcance, espaço de canal, resistência de canto e estabilidade de engate para um recurso complexo. Nessa situação,Ferramentas de fresagem personalizadaspode ser avaliado em torno do recurso real e do padrão de falha. A opção personalizada ainda deve ser validada através de ensaios controlados; a personalização não elimina a necessidade de corrigir a instabilidade da configuração. Uma sequência controlada de solução de problemas Quando for encontrado desgaste irregular do canal, use a seguinte ordem para evitar alterar diversas variáveis ​​ao mesmo tempo: Preservar e inspecionar a ferramenta com falha. Fotografe cada canal e registre o tempo de corte ou contagem de peças. Identifique se o dano é desgaste, lascas, aresta postiça, fricção ou uma combinação. Limpe e inspecione a haste, a pinça, o suporte, a interface do fuso e as superfícies de assentamento da ferramenta. Meça o desvio usando o procedimento normal, o mais próximo possível da aresta de corte. Verifique a projeção da ferramenta, o engate axial, o engate radial e as condições reais de entrada e saída. Confirme a fixação e o suporte do trabalho, especialmente perto de paredes finas, lacunas ou áreas interrompidas. Inspecione o formato e o escoamento dos cavacos. Procure chips embalados ou evidências de recortamento. Revise a classe do material, a geometria da ferramenta, o revestimento, o método de refrigeração e os dados de corte. Altere uma variável principal e execute uma comparação controlada. Registre o resultado antes de fazer outra alteração. Os parâmetros de corte devem ser tratados como referências iniciais para a ferramenta e aplicação exatas. Eles devem ser validados na máquina, suporte, fixação e classe de material específicos antes de serem adotados como um processo padrão. Solução de problemas por padrão de desgaste Uma flauta apresenta grande desgaste no flanco Verifique primeiro a excentricidade, o assentamento da ferramenta, a condição da pinça e o engate do percurso. Confirme se o canal sobrecarregado não está entrando repetidamente em um canto ou região de cavacos compactados. Uma flauta está lascada enquanto as outras parecem utilizáveis Inspecione as condições de impacto, estoque interrompido, estratégia de entrada e saída, desvio do suporte e movimento da peça. Se a falha se repetir no mesmo local do caminho, revise essa transição no programa CAM e na peça. Uma flauta tem borda acumulada Procure atrito, espessura de cavacos desigual, evacuação insuficiente de cavacos e problemas de adesão específicos do material. Revise a nitidez da borda, o polimento do canal, a lubrificação e o revestimento somente após verificar a carga desigual. Todas as flautas apresentam desgaste, mas uma é muito pior Este padrão pode indicar uma carga geral do processo combinada com desvio ou desvio. Revise os dados gerais de engate e corte e, em seguida, verifique por que um canal está carregando a carga adicional. O desgaste varia entre as peças Fixação inconsistente, variação de estoque, condição do material, empacotamento de cavacos ou mudanças térmicas podem estar levando o processo para dentro e para fora da estabilidade. Registre a localização da peça e o momento em que a diferença de desgaste aparece. Erros comuns a evitar Substituir a ferramenta sem verificar o suporte Uma nova ferramenta no mesmo suporte instável pode reproduzir o mesmo padrão de desgaste. Verifique toda a cadeia de fixação da ferramenta antes de concluir que a ferramenta está com defeito. Reduzir o avanço como única correção Uma redução de alimentação pode ocultar o sintoma temporariamente, ao mesmo tempo em que deixa o desvio, a fricção ou o impacto inalterados. Também pode criar espessura insuficiente de cavacos e mais calor. Culpar o revestimento antes de examinar o carregamento O revestimento não pode fazer com que todos os canais compartilhem a carga quando há desvio ou deflexão. Diagnosticar a causa mecânica antes de selecionar um revestimento diferente. Ignorando a posição do canal da ferramenta com falha A posição da flauta danificada é uma evidência útil. Registre-o de forma consistente em vez de descartar a ferramenta sem inspeção. Alterando velocidade, avanço, geometria e refrigeração juntos Múltiplas alterações simultâneas tornam o resultado difícil de interpretar. Use ensaios controlados e documente uma mudança primária de cada vez. Perguntas frequentes O que faz com que um canal de uma fresa de topo de metal duro se desgaste mais rapidamente que os outros? As causas comuns incluem desvio radial, mau assentamento da ferramenta, pinça desgastada, projeção excessiva, engate desigual, movimento da peça, empacotamento de cavacos e vibração. Inspecione a configuração completa antes de assumir um defeito de metal duro ou revestimento. O desvio da fresa de topo pode causar lascamento? Sim. O desgaste pode sobrecarregar uma flauta e deixar outra flauta esfregando. A aresta sobrecarregada pode lascar ou desgastar-se rapidamente, especialmente durante corte interrompido, engate em toda a largura ou operações com evacuação limitada de cavacos. Devo trocar o revestimento quando um canal apresenta arestas postiças? Não imediatamente. Primeiro verifique o desvio, a afiação da aresta, a espessura dos cavacos, o escoamento dos cavacos, a lubrificação e a compatibilidade do material. Uma mudança de revestimento pode ajudar apenas quando o mecanismo de falha dominante corresponder à função pretendida do revestimento. Como posso saber se o desgaste irregular é causado por trepidação ou excentricidade? A excentricidade geralmente produz um desequilíbrio consistente entre canais, enquanto a vibração tende a criar marcas de vibração repetidas e pode variar com o engate ou a velocidade do fuso. Ambos podem coexistir, portanto inspecione a ferramenta, o suporte, o suporte da peça e o padrão de superfície juntos. Que informações devo fornecer ao solicitar uma recomendação de solução de problemas? Forneça a classe do material, diâmetro da ferramenta e contagem de canais, alcance e balanço, tipo de suporte, desvio medido, se disponível, parâmetros de corte, engate radial e axial, método de refrigeração, detalhes de fixação, contagem de peças e fotografias nítidas de cada canal. Conclusão O desgaste irregular do canal não é apenas um problema de substituição de ferramenta; é uma prova de que a carga de corte não está a ser partilhada conforme pretendido. Excentricidade, assentamento da ferramenta, condição do suporte, projeção excessiva, movimento da peça, alterações de engate, empacotamento de cavacos e vibração devem ser considerados antes de alterar a classe ou revestimento da ferramenta. Uma sequência de correção confiável preserva a ferramenta com falha, identifica o padrão de desgaste, verifica a cadeia de fixação da ferramenta, verifica o engate e a fixação e altera uma variável principal de cada vez. Se o processo ainda exigir um equilíbrio especial de alcance, espaço de cavaco e resistência da aresta, uma ferramenta projetada especificamente poderá ser avaliada depois que a configuração básica estiver estável. Se sua fresa de topo de metal duro apresentar desgaste de um canal, lascamento repetido, aresta postiça ou vida útil da ferramenta instável,Contato Supalcom a classe do material, ferramenta atual, detalhes do suporte e do balanço, dados de corte e fotografias de cada canal. Essas informações ajudam a identificar uma geometria prática e um ponto de partida do processo para validação na máquina.

2026

10/13

Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.
2026

10/01